Satisfactory Production Ratios & Efficiency Guide
Understand Satisfactory 1.2 production ratios using per-minute rates, bottlenecks, clock speeds, transport throughput, manifolds and byproduct handling.
Production efficiency in Satisfactory comes down to matching rates. Every recipe states how many items or cubic metres a machine consumes and produces per minute. Once those numbers are compared, factory ratios become arithmetic rather than guesswork.
Work in items per minute
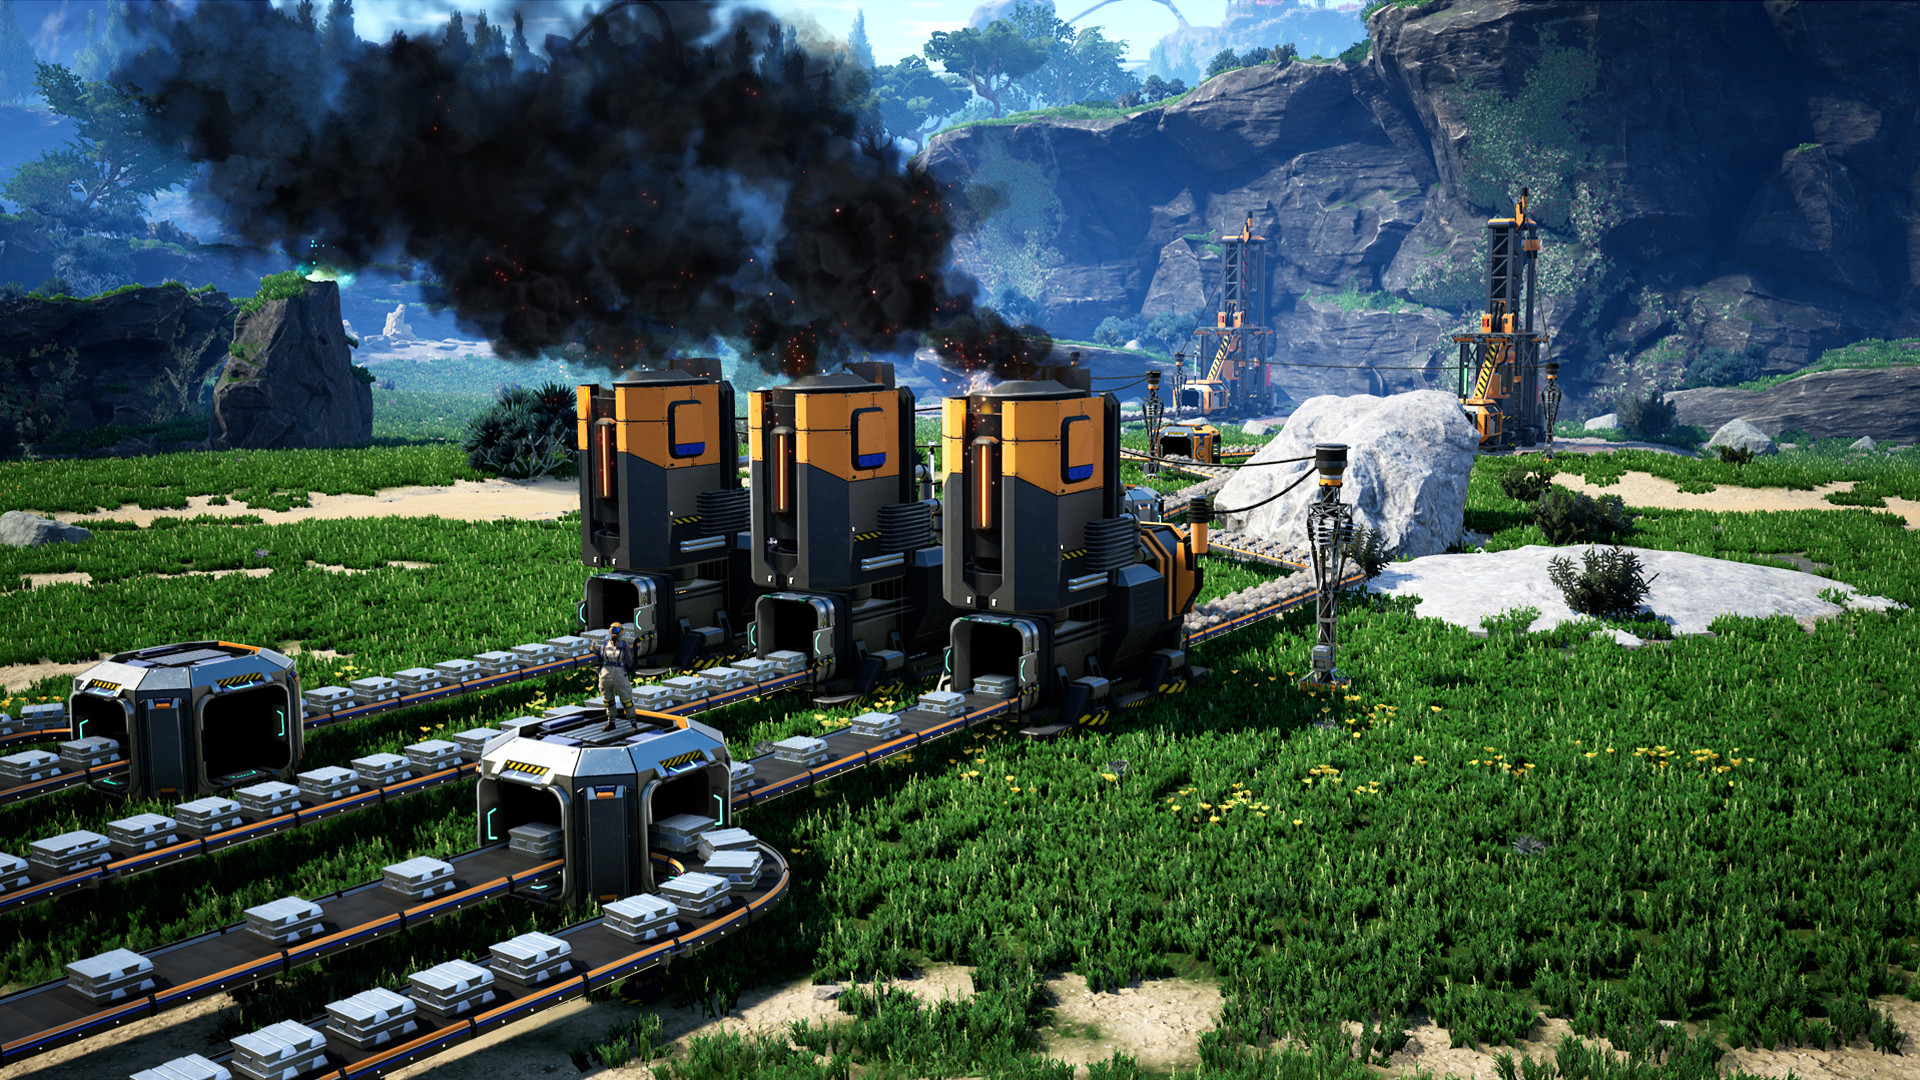
Use the per-minute rates shown on machines and recipes as the common unit. If a Smelter outputs 30 Iron Ingots/min and a Constructor recipe needs 30 Iron Ingots/min, one Smelter can feed one Constructor for that recipe. If the consumer needs 60/min, you need twice that supply or a different clock-speed arrangement.
Find the bottleneck first
A production line can only sustain the rate of its slowest required input or transport stage. Check miner output, belt throughput, pipe throughput and machine demand before adding more production buildings. Extra machines do not create extra resources by collective optimism.
Underclock for exact ratios
Machines do not need to run at 100%. Underclocking lets a machine consume and produce exactly the rate required by the next stage while reducing its power demand. This is useful when the ideal ratio would otherwise require a fraction of a machine.
Overclock where it solves a real constraint
Power Shards allow production buildings and resource extractors to run above their normal clock speed. Overclocking can save space or increase output from a limited resource node, but it increases power demand disproportionately. Compare the benefit with the available power margin before using it everywhere.
Transport throughput is part of the ratio
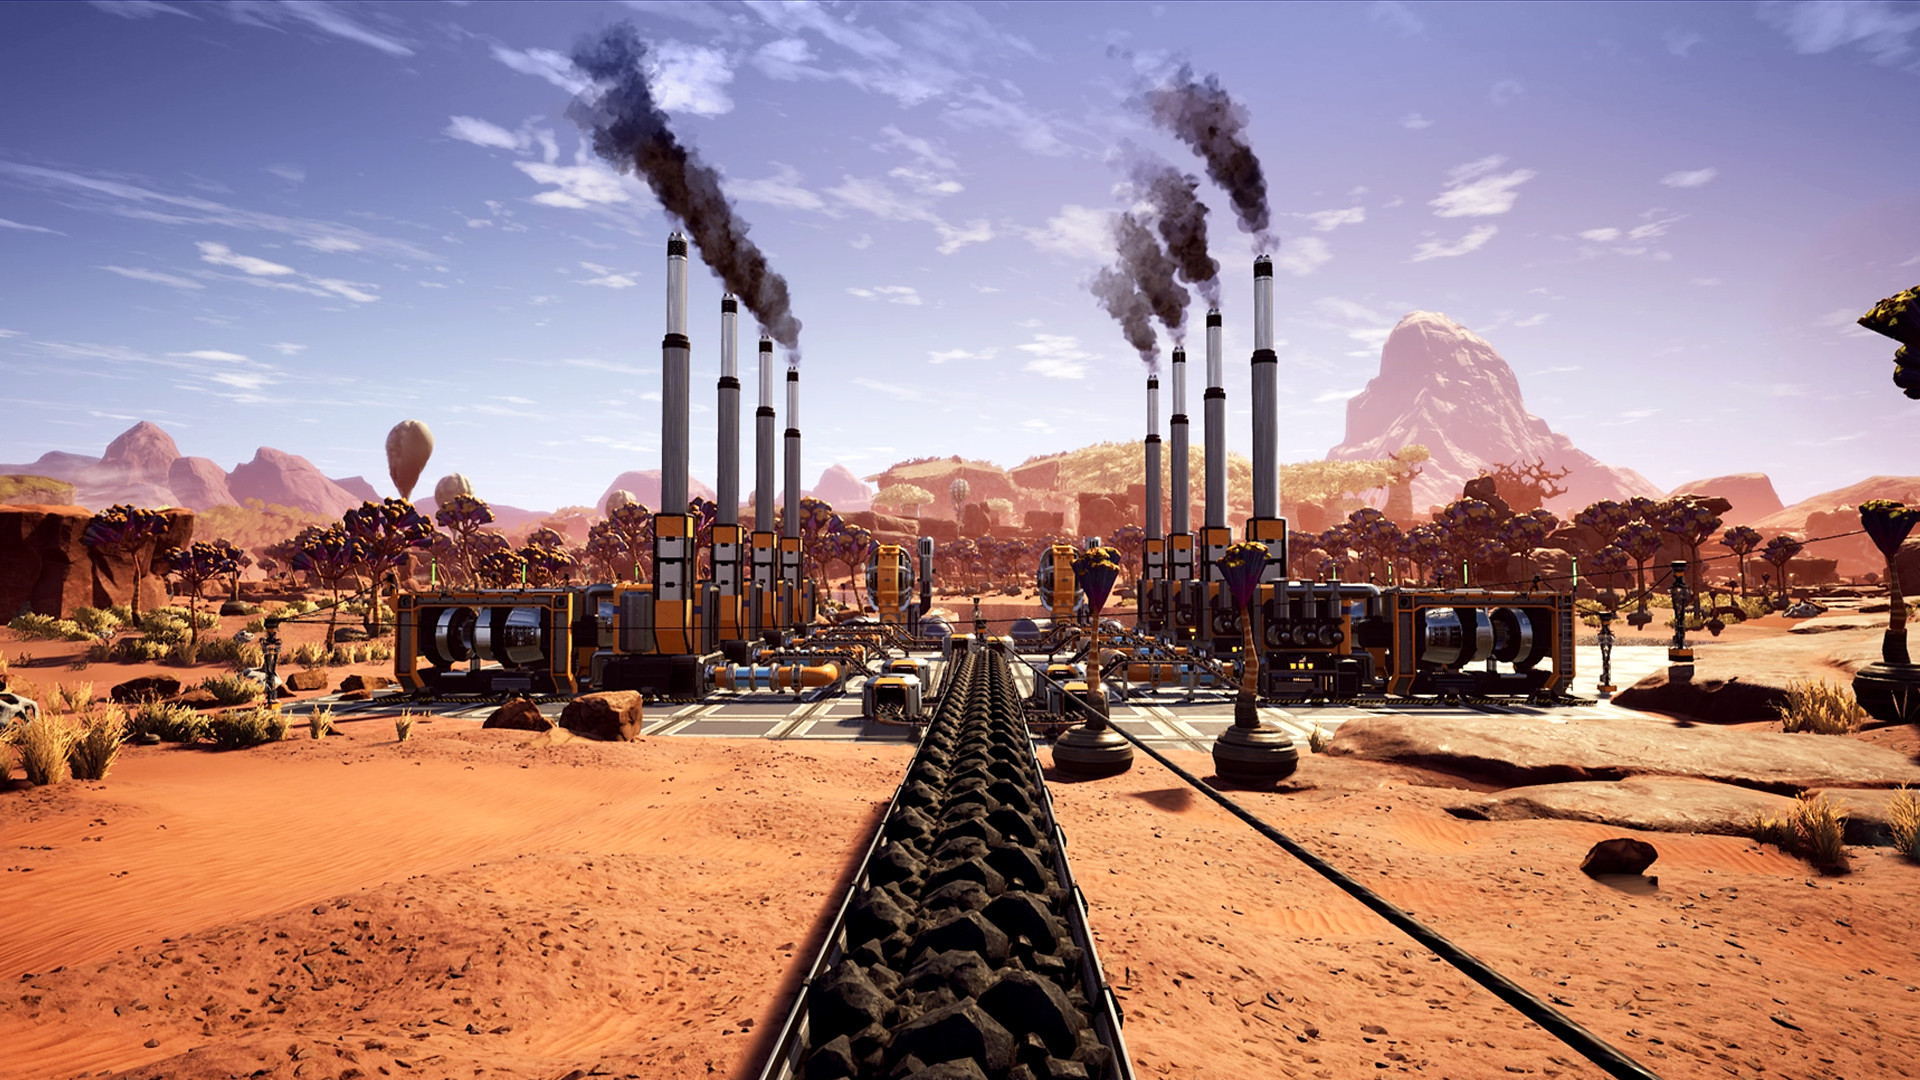
Production math is meaningless if the belt or pipe cannot carry the calculated flow. Check the capacity of the conveyor or pipeline segment that all material must pass through, particularly after mergers and before large manifolds.
Manifolds reach steady state
A correctly supplied manifold can operate at full efficiency once upstream machines and buffers have filled. During startup, the first machines may take most of the input while later machines wait. That temporary behaviour does not necessarily mean the final ratio is wrong.
Buffers do not fix a bad ratio
Storage Containers and Fluid Buffers can smooth temporary fluctuations and make troubleshooting easier, but they cannot permanently compensate for a production deficit. If consumption exceeds supply, the buffer will eventually empty; if production exceeds consumption, it will eventually fill.
Account for byproducts
Oil and aluminium production can stop when a byproduct output fills. Efficiency therefore includes keeping every required output moving, not merely supplying the main input. Heavy Oil Residue, Polymer Resin and recycled Water are common examples where output handling affects the entire chain.
Use efficiency displays as diagnostics
If a machine repeatedly stops, identify whether it is waiting for input, blocked by output, short of power or affected by logistics. Fix the actual cause before changing clock speeds or adding machines.
Optimise after the line works
Build a stable baseline using standard recipes, then consider alternate recipes and clock-speed changes. Alternate recipes can transform resource requirements, so a mathematically perfect factory based on one recipe set may become obsolete when a better combination is unlocked.
Worked example: turn 60 Iron Ore/min into two useful products
A Miner Mk.1 on a normal Iron Ore node produces 60 Ore/min at 100% clock speed. Two Smelters consume 30 Ore/min each and together produce 60 Iron Ingots/min.
- Plates: send 30 Iron Ingots/min to one Constructor for 20 Iron Plates/min.
- Rods: send the remaining 30 Iron Ingots/min to two Constructors, each using 15 Ingots/min to produce 15 Rods/min.
- Result: 20 Plates/min plus 30 Rods/min without wasting the ingot supply. The incoming 60 Ore/min fits exactly on a Mk.1 conveyor belt.
For the build order and troubleshooting, see the Getting Started Guide.
Worked example: standard steel without leftover ingots
Two Foundries need a combined 90 Iron Ore/min and 90 Coal/min, producing 90 Steel Ingots/min. One Steel Beam Constructor requires 60 Ingots/min and produces 15 Beams/min. One Steel Pipe Constructor uses the remaining 30 Ingots/min and produces 20 Pipes/min.
Machine count: 2 Foundries + 2 Constructors. A belt carrying all 90 merged ingots must be Mk.2 or faster because Mk.1 is limited to 60 items/min. Separate feeds can instead be designed to avoid a single 90/min segment. See the Steel Production Guide for the construction sequence.
Worked example: coal-generation capacity
Eight full-speed Coal-Powered Generators require 8 × 15 = 120 Coal/min and 8 × 45 = 360 m³ Water/min, and generate 8 × 75 = 600 MW gross. Three Water Extractors provide 360 m³/min while drawing 60 MW combined. The 540 MW remainder is before miner, pumps and other site power costs.
A Mk.1 pipe can transport up to 300 m³/min, so splitting or injecting the water feed is essential. The Coal Power Guide explains startup and common failure patterns.
Quick transport-capacity reference
- Conveyor Mk.1: 60 items/min
- Mk.2: 120 items/min
- Mk.3: 270 items/min
- Mk.4: 480 items/min
- Mk.5: 780 items/min
- Mk.6: 1,200 items/min
- Pipeline Mk.1: 300 m³/min; Mk.2: 600 m³/min
A nominal capacity is a maximum for a segment, not a guarantee that fluid will maintain that flow through a poorly arranged network. Account for head lift, pipe routing and startup conditions.
How to adapt these numbers
For a target output rate, divide the required items/min by the output of one machine/min. Round up to a whole number of machines, or use underclocking when available. Then repeat upstream to calculate the input materials and check every conveyor and pipeline section for bottlenecks. These examples use standard recipes and 100% clock speed; alternate recipes can substantially change the result.
Verification sources: Conveyor Belts, Pipelines and the official wiki recipe pages. For extensive alternate-recipe comparisons, use Satisfactory Tools rather than treating this page as a replacement for a full production-chain calculator.